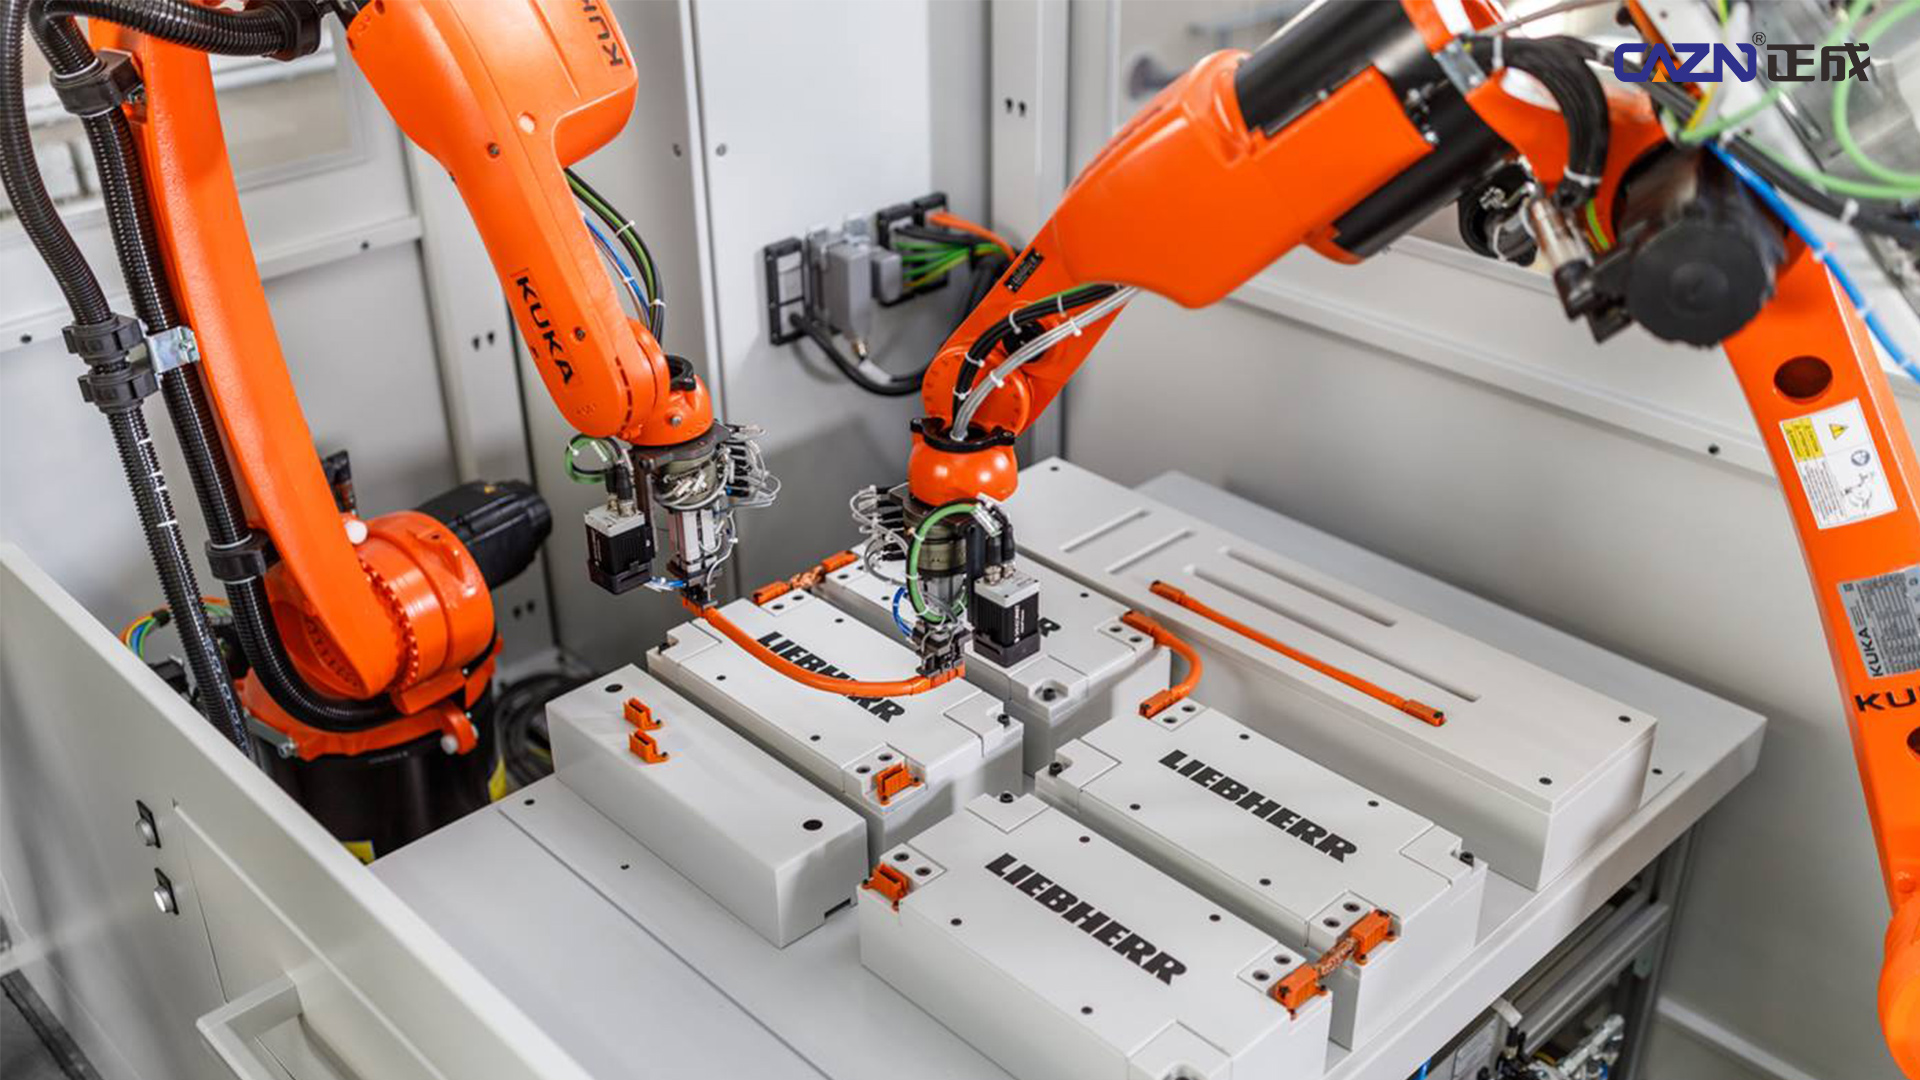
1. Industrial Connectivity Challenges in Advanced New Energy Battery Manufacturing
Driven by the rapid growth of the electric vehicle and energy storage industries, lithium-ion and sodium-ion battery manufacturing is entering the terawatt-hour (TWh) era. From cell sorting, module loading, and laser welding of battery tabs to BMS harness installation and end-of-line (EOL) charge-discharge testing of complete battery PACKs, highly automated, takt-driven assembly lines place demanding requirements on industrial equipment, including industrial robots, precision laser welding machines, high-speed machine vision inspection systems, automated guided vehicles (AGVs), and testing workstations.
Modern power battery PACK production lines often target cycle times of 30–60 seconds. In high-throughput manufacturing environments characterized by strong electromagnetic interference (EMI) and continuous high-speed operation, industrial connectors and cables must withstand considerable mechanical and electrical stress.
High-frequency flexing and torsion in drag chains and robotic joints
During the rapid, repetitive movements of six-axis industrial robots used for battery cell handling and welding, cables installed in drag chains and robot arms must withstand millions of bending, twisting, and tensile cycles. Ordinary cables may develop conductor fatigue and breakage, shielding-layer fractures that compromise electromagnetic protection, or cracked outer jackets. These failures can trigger unexpected production line stoppages.
Severe EMI from laser welding and high-power servo drives
Battery PACK production lines frequently use kilowatt-class fiber lasers for copper and aluminum battery-tab welding, while multiple high-power servo motors accelerate and decelerate at high frequency. Electromagnetic pulses and harmonic interference can couple into industrial bus cables and machine vision signal lines, potentially causing Industrial Ethernet packet loss, image artifacts from industrial cameras, or inaccurate measurement data.
High-frequency mating wear in EOL testing stations
During electrical performance and insulation withstand-voltage testing, quick-connect test interfaces may be mated and unmated hundreds or even thousands of times per shift. Ordinary industrial terminals with limited mating durability can experience contact-plating wear and increased contact resistance, potentially producing false test failures and inaccurate battery PACK acceptance results.
Metallic spatter and welding fume contamination
Fine metallic particles generated during laser welding, together with airflow and pressure differences created by dust extraction systems, place stringent demands on connector sealing, dust protection, and the thermal resistance of insulating housings.
2. Key Technical Requirements for High-Reliability Connectors and Cables in Battery Manufacturing Equipment
To support demanding equipment availability targets, such as an overall equipment effectiveness (OEE) target of 90% or higher, Shenzhen CAZN Electrical Co., Ltd. (CAZN) provides connector and cable solutions designed for high-flexibility applications, EMI resistance, and extended mating life.
High-Flex Drag Chain Cables and Integrated Overmolding
Ultra-fine stranded oxygen-free copper conductors
Each conductor can be constructed from finely stranded, high-purity oxygen-free copper wires with individual wire diameters of approximately 0.05–0.08 mm. Combined with low-friction modified TPE or PP conductor insulation, this construction can reduce internal mechanical stress and improve flexibility under repeated movement.
Abrasion-resistant PUR outer jackets
High-mechanical-strength polyurethane (PUR) jackets offer resistance to mineral oils, coolants, and cutting fluids, depending on the material formulation. For demanding drag chain applications, the cable design can target continuous flexing endurance of at least 10 million cycles, subject to the specified test conditions and validation results.
Integrated injection-molded strain relief
The connector tail and PUR cable jacket can be integrated through secondary vertical injection molding to create a continuous interface with graduated strain relief. This helps reduce stress concentrations at the cable exit and minimizes the risk of damage caused by sharp bending near the connector.
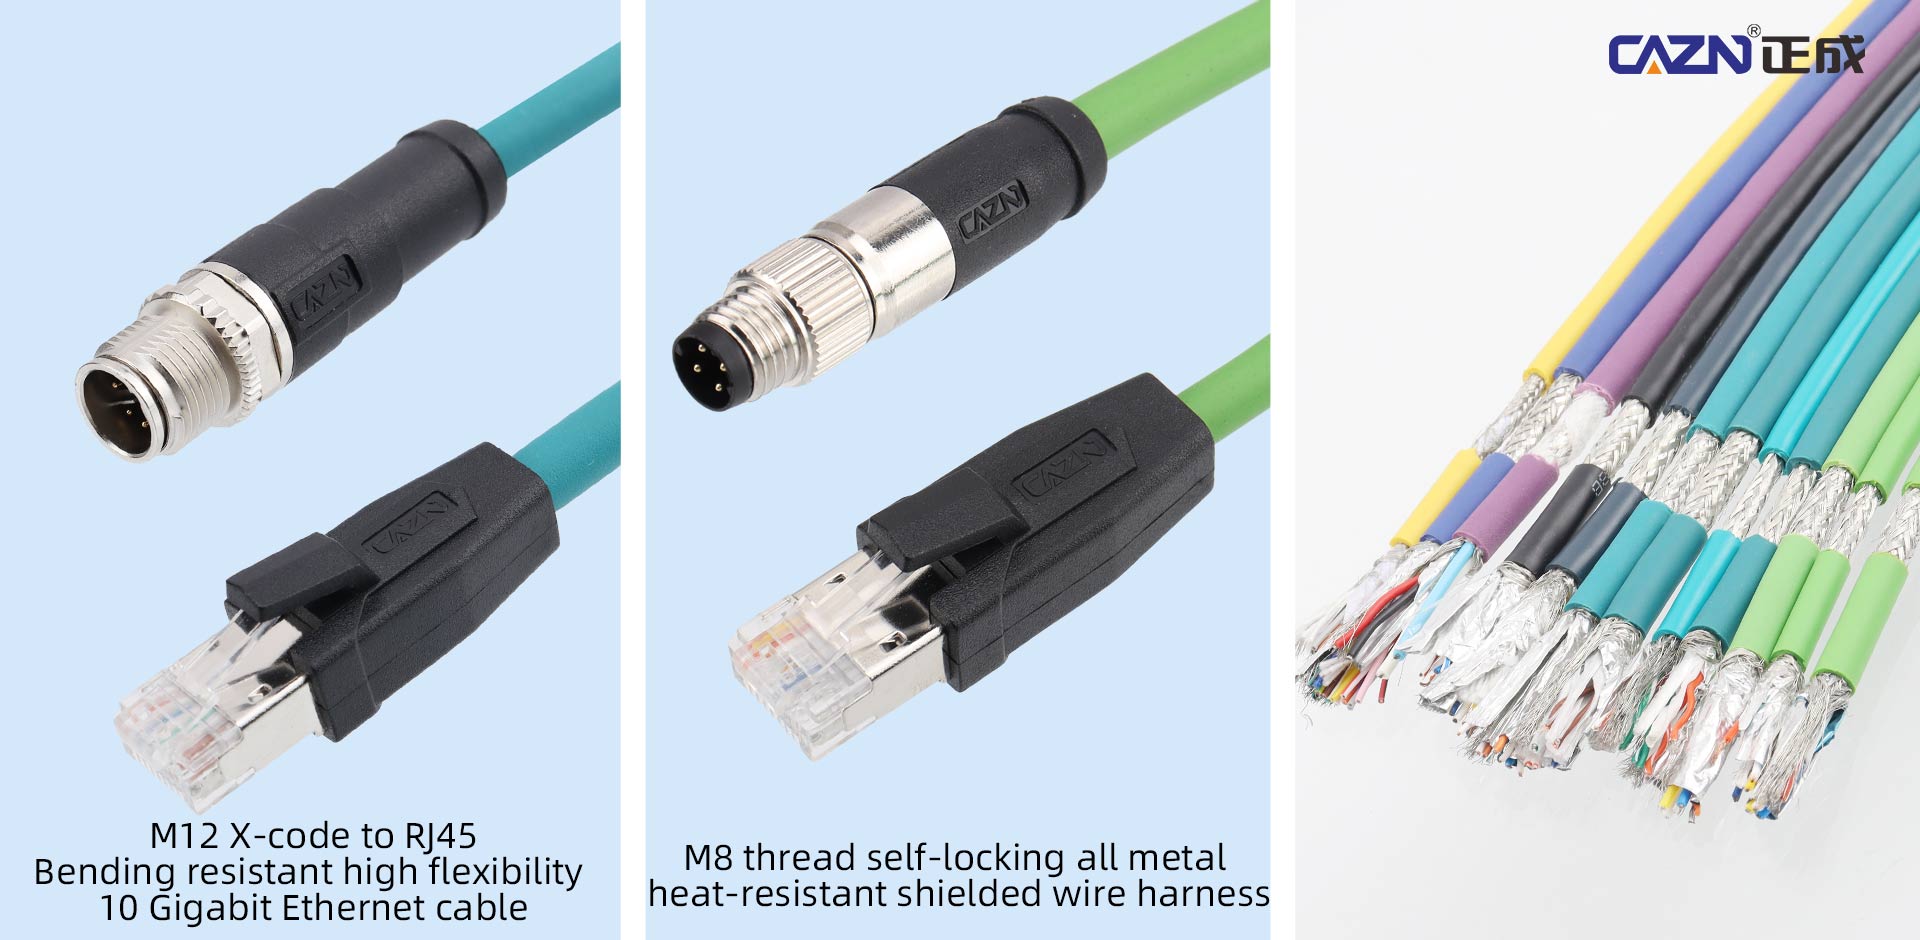
High-Speed Machine Vision and Industrial Ethernet Connectivity: M12 X-Coded and D-Coded Connectors
360-degree shielded construction
M12 X-coded connectors use an internal metallic cross-divider to physically separate the four twisted pairs. This structure helps control near-end crosstalk (NEXT) and far-end crosstalk (FEXT), supporting Cat 6A-class cabling and data transmission rates of up to 10 Gbps when the complete channel meets the relevant requirements.
Robust zinc-alloy die-cast housings
Zinc-alloy die-cast housings can provide mechanical protection and contribute to electromagnetic compatibility (EMC). Shielding effectiveness depends on the complete connector and cable assembly, including shield termination, mating interfaces, and installation. Performance targets such as attenuation exceeding 50 dB at 500 MHz should be verified through product-specific test reports rather than assumed for every model.
These design features help protect machine vision and industrial communication links against interference from high-power laser equipment and high-frequency inverters.
Wear-Resistant Gold-Plated Contacts and Long-Life Test Connections
Thick hard-gold plating
Contact pins can use spring-grade beryllium copper or phosphor bronze substrates, with a nickel underlayer and hard-gold plating approximately 30–50 microinches thick (0.76–1.27 μm), depending on the contact specification. A properly engineered contact system can target 5,000 or more mating cycles while maintaining stable contact resistance under defined test conditions.
Floating blind-mate mechanisms
Test interfaces can incorporate a floating, self-aligning mechanism with axial compensation of ±2 mm and radial compensation of ±1.5 mm. This helps accommodate minor positioning errors in automated handling equipment and fixtures, reducing the risk of bent contacts and mechanical damage during repeated mating.
3. Comparison of Industrial Connector and Cable Solutions for Battery PACK Production Lines
|
Key Performance Indicator |
Standard Commercial Cables |
General Industrial Cables |
CAZN High-Flex Shielded Cable Assemblies for Battery Equipment |
|---|---|---|---|
|
Drag chain flex life |
Typically below 500,000 cycles in lower-grade designs |
Approximately 2–5 million cycles for some designs |
Target of 10 million cycles or more for validated configurations |
|
Gigabit machine vision EMI protection |
May experience interference-related packet loss or image disruption |
Single-layer aluminum foil shielding may be insufficient in demanding high-frequency environments |
Dual shielding using aluminum foil and an 85% tinned-copper braid, with 360-degree shield termination |
|
Oil and spatter resistance |
PVC jackets may deteriorate when exposed to incompatible oils or chemicals |
Standard PUR provides application-dependent resistance |
Specialized flame-retardant, abrasion-resistant, oil-resistant PUR formulations for suitable environments |
|
Connector mating durability |
Varies by product; lower-grade terminals may have limited durability |
Often approximately 200–500 cycles for selected products |
Configurations targeting 500–5,000 or more cycles, depending on contact design and plating |
|
Ingress protection |
Some products provide only IP20 protection |
About Author
|